Design guide for impact-resistant polycarbonate exterior glazing
Practical guide for impact-resistant polycarbonate exterior glazing: load assumptions, edge processing, fastening, sealing, ageing reserves, testing and validation.
Classification and purpose of this design guide
Impact-resistant polycarbonate exterior glazing is used in industry where high energy input, exposure to the weather and low masses are unavoidable. Typical applications are machine guard windows in outdoor areas, roof and façade elements, housing covers, vehicle glazing for commercial vehicles and enclosures in harsh environments. The aim is a robust, long-lasting and optically flawless solution with plannable maintenance and calculable service lives.
Compared with glass, polycarbonate offers significantly higher impact resistance at low weight, but is more sensitive to scratches, chemicals and notch-inducing geometries. This guide structures the design along load assumptions, material and surface selection, edge processing, fastening and sealing concepts as well as the definition of sensible ageing reserves.
Material fundamentals and surface options
Impact resistance, notch sensitivity and optical requirements
Polycarbonate is an amorphous thermoplastic with very high energy absorption in the impact test and good transparency. For the design it is crucial that notches, sharp internal radii and rough edges increase the local stress intensity and thus reduce the effective impact resistance. A low-notch design, sufficiently large internal radii and high-quality edges are therefore an integral part of the design.
In optically relevant areas, distortion due to residual stresses must be avoided. Uniform bearing pressures, defined clamping lengths and a homogeneously machined surface reduce double images, Newton rings and local scattering. For material selection and optical assessment, the overview of transparent engineering plastics helps as a guide.
UV protection and hard coating
Exterior glazing benefits from UV-stabilised formulations and surface coatings. Hard coatings increase scratch resistance and can improve cleanability. Selection and coating system depend on the stress profile, optical requirements and cleaning regime. The comparison of hard coatings for PC and PMMA shows typical strengths and limits of various systems. Practical aspects of integration in the component structure are illustrated by hard-coated polycarbonate sheets in practice.
UV and weather resistance are central for outdoor use. Information on selecting suitable materials and additive packages is provided by the article resistant plastics against UV radiation as well as the overview of transparent engineering plastics in outdoor areas.
Load assumptions and design strategy
Continuous surface loads and wind loads
Essential design loads are stationary surface loads due to wind, vacuum or overpressure in enclosures as well as snow or ice accumulation. For the design, a combination of static and quasi-static load cases is applied. The permissible deflection depends on the visual requirement, the sealing concept and any risk of collision with adjacent components. Load distribution, support conditions and edge distances largely determine the stresses in the sheet.
Since environmental effects vary, the design scenario is defined on a project-specific basis. Load collectives can include seasonal or event-based peaks. For reliable results, conservative partial safety concepts are combined with realistic load assumptions.
Point loads and impact energy
In addition to surface loads, local point loads and impact energy are critical. Typical scenarios are gravel impact, tool impact or operating errors. Impact safety depends on sheet thickness, support, edge quality and surface condition. A sufficiently dimensioned edge bond, large-area load transfer and low-notch details increase the energy reserves. For recurring impact stress, test component trials are expedient.
Temperature, moisture and creep
Temperature changes, moisture absorption and long-term loads influence stiffness and stress level. The thermal expansion of the material requires a sliding, low-stress support. Creep under permanent clamping pressure or bolt preload must be taken into account in the sealing layout. Supplementary information on cyclic conditions can be found in the article resistance to temperature changes.
Permissible deflection, visual and sealing criteria
The permissible deflection results from optical requirements, the sealing geometry and functional limits. Viewing windows with high reading accuracy tolerate lower deflections than purely protective panels. Seals must accommodate movements without losing sealing pressure or position. A clear acceptance clause with limit samples or measurement points saves time during approval.
A continuous design procedure has proven its worth:
- Define load collectives and specify support conditions.
- Pre-dimension sheet thickness and geometry for deflection and stress.
- Execute edge and hole details with low stress.
- Check the fastening and sealing concept for movement accommodation and creep.
- Specify surface options, define the cleaning regime.
- Carry out component tests and validation with safety reserves.
Thickness selection, geometry and shaping
Sheet thickness and beads
The thickness selection results from deflection limits, impact requirement and fastening grid. Larger spans or higher loads require either more thickness or stiffness-increasing geometries. Optionally, beads, ribs or curved surfaces can be integrated, which increase stiffness without excessive gain in mass.
For optically demanding viewing windows, a homogeneous thickness with low residual stress is advantageous. Temperature fields and local bearing pressures must not produce visible distortion. Information on reproducible forming quality is contained in Quality assurance in thermoforming transparent components.
Curvatures, preload and thermoforming
Slight curvatures increase inherent stiffness and can reduce deflection. For thermoformed discs, heating profiles, tool radii and cooling conditions must be selected so that optical distortion remains minimal. A defined stress relief after machining reduces residual stresses and improves crack resistance.
Edge processing and stress management
Machining and laser processing
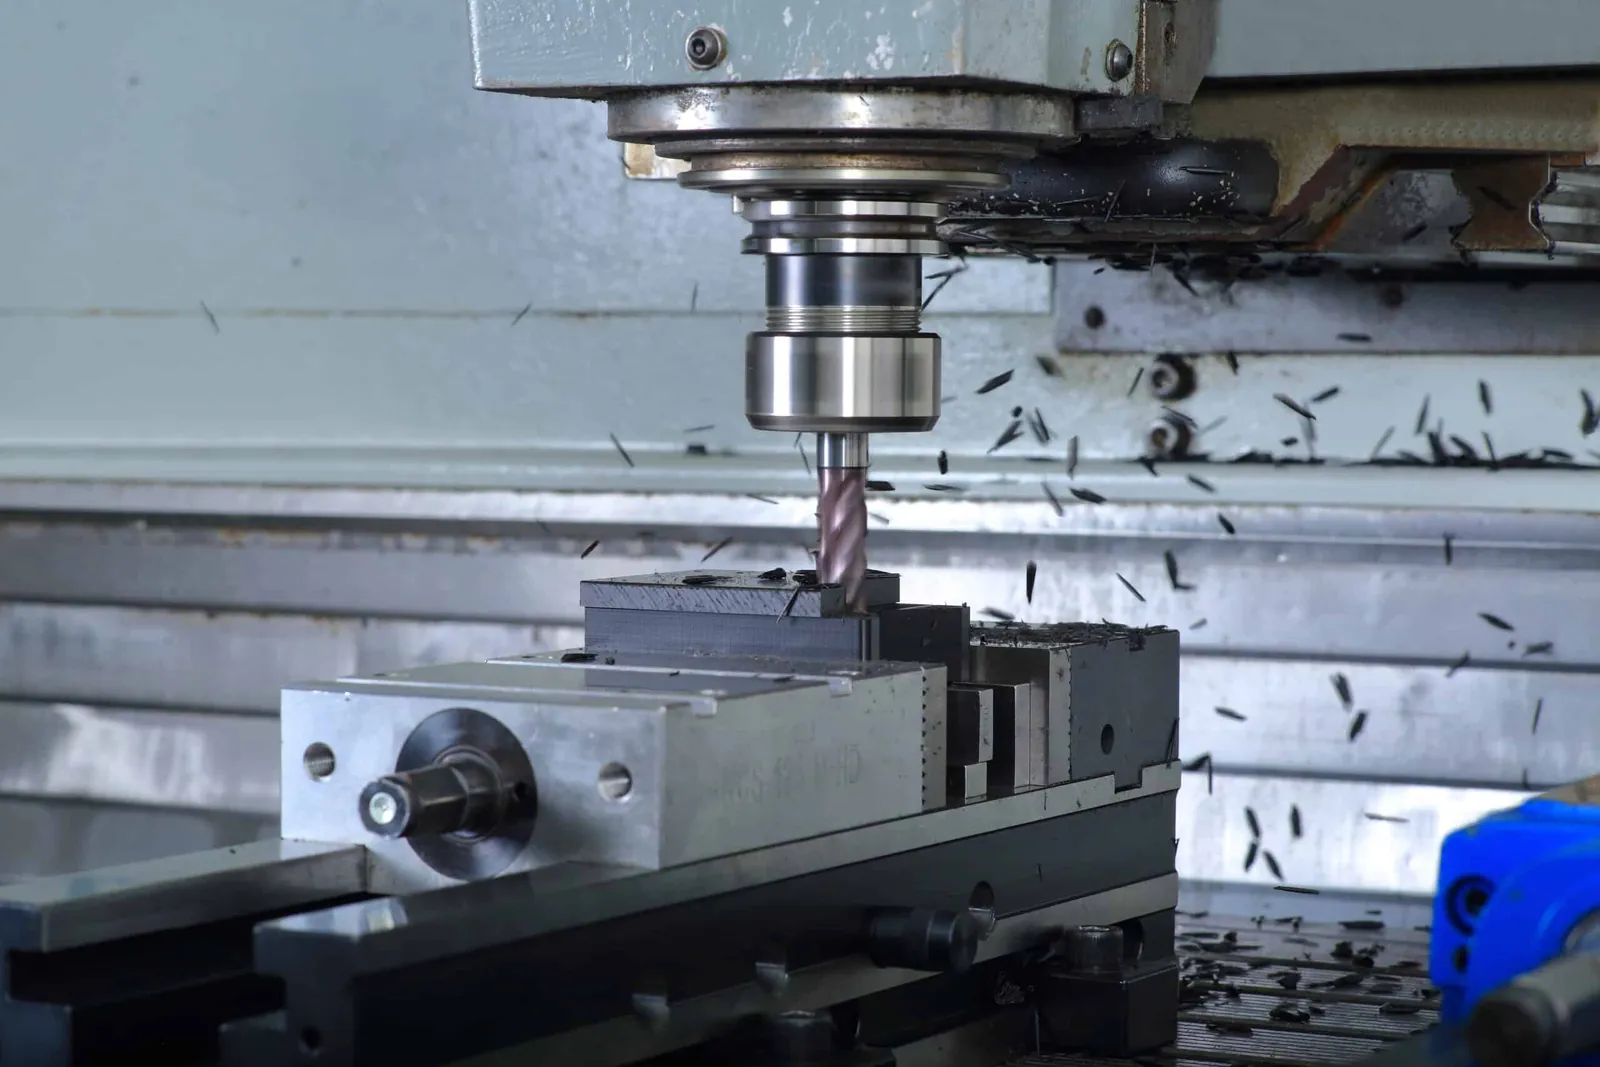
Edge quality controls notch sensitivity. Milling with sharp tools, sufficient chip removal and a suitable cutting speed delivers reproducible results. Sawn edges must be reworked to reduce micro-notches. Laser processing of transparent plastics can produce smooth edges, but requires process validation with regard to heat input and residual stresses.
In plastic machining the following applies: cooling, sharp tools, low vibration and matched feed rates minimise microcracks. Polishing improves the appearance, but must not produce heat cracks.
Edge quality, deburring and polishing
A step-by-step rework process with deburring, fine grinding and optional polishing produces a low-notch geometry. Sharp internal edges must be rounded, external edges are lightly broken. Polished visible edges are visually appealing, but mechanically a fine ground finish is often sufficient, provided the notch effect is eliminated.
Internal radii, holes and edge distances
Holes are made centred, with sufficient distance from edges and other penetrations. Internal radii instead of sharp corners distribute stress peaks. The aim is a load-path-compliant geometry with low stress concentrations. After drilling, chips and cooling lubricant must be removed thoroughly to avoid stress cracks.
Fastening and sealing concepts
Clamping frames and floating support
Clamping frames distribute bearing forces over a large area and enable a floating support that accommodates thermal changes in length. Soft-elastic intermediate layers protect the surface and ensure uniform pressure. The length of the clamping area and the distribution of force introduction must be selected so that local stresses remain limited.
Bolted connections, washers and slotted holes
Bolted connections require large-area washers or sleeves to avoid point loads. Slotted holes or sliding bushes permit thermal changes in length and reduce constraint stresses. Preloads must be defined so that the sealing pressure is maintained in the long term without excessively compressing the material.
Seals and adhesives, material compatibility
Sealing materials such as EPDM, neutral-curing silicone or TPE are frequently used. What matters is UV resistance, low outgassing, a suitable hardness and a low tendency to plasticiser migration. For material selection and design, the guide to selecting sealing materials provides support.
For bonded joints, chemical resistance and the risk of stress cracking must be expected. Solvent-based systems can trigger stress cracks. Preference should be given to tested, material-compatible adhesives and primers with assured ageing performance. Cleaning processes that could conflict with the sealing concept must be specified in advance. Information for operation is provided by cleaning and care of transparent plastic glazing.
Ageing reserves and service life planning
UV, weather and media exposure
UV radiation, temperature changes, moisture, de-icing salts, cleaning chemicals and industrial atmosphere influence the service life. Conservative planning takes into account decreasing impact resistance and increasing notch sensitivity over time. Additive UV stabilisation and suitable surface solutions increase the reserves. In-depth background is provided by ageing processes in plastics and high-performance plastics in outdoor areas.
Safety factors, monitoring and replacement concept
For recurring inspections, visual test criteria, permissible scratch patterns, limits for haze and simple function tests are practical. A plannable replacement window is derived from the usage scenario, stress, maintenance and optical requirements. Spare parts stocking, replacement tools and seal sets belong in the concept.
Quality assurance, testing and approval
Component tests, impact tests and leak testing
Component validation is based on the real load collective. Relevant building blocks are leak tests, impact tests with representative energy inputs, pressure and suction loads as well as temperature change tests. Test setups take into account the support, sealing system and realistic preloads.
Dimensional accuracy and visual inspection
Manufacturing tolerances, run-out, flatness and optical quality are checked with defined measuring methods. Typical defect patterns are edge cracks, hole pull-outs, surface scratches or distortion due to inhomogeneous bearing pressures. An incoming goods inspection with documented limit samples reduces later discussions.
Documentation and conformity
The project documentation comprises the material specification, coating data, machining parameters, assembly instructions, test reports and approval records. For industry-specific requirements, a comparison with standards and approvals for engineering plastics is recommended in order to define test scopes and evidence in a targeted manner.
Frequently asked questions
How can the thickness of PC exterior glazing be determined in a practical way without standard specifications?
Procedure via requirements analysis, load assumptions and deflection criterion, then variant calculation with support conditions. The preferred variant is validated in component tests with real supports and seals.
Which sealing materials are particularly compatible with polycarbonate?
EPDM, TPE and neutral-curing silicones have proven their worth. What matters is UV resistance, suitable hardness, low plasticiser content and tested chemical compatibility. A material test against media in the case of use is advisable.
How are bolted connections designed so that thermal changes in length do not cause cracks?
With large-area washers or sleeves, defined preloads and slotted holes in the longitudinal direction. Sliding intermediate layers and a floating bearing concept reduce constraint forces.
Are hard coatings required for every exterior glazing?
Not necessarily. They increase scratch resistance and can improve cleanability. Whether the added benefit justifies the cost depends on stress, visual requirements, cleaning regime and maintenance intervals.
How are stress cracks caused by cleaning and media contact avoided?
Through material-compatible cleaning agents, soft cloths, adapted intervals and avoiding solvents. Seals and adhesives must be checked for chemical compatibility in order to avoid stress cracks.
Can polycarbonate be thermally tempered like glass?
Tempering as with glass is not possible. What makes sense are stress-relief processes via thermal relaxation after machining as well as a low-notch design so that local stress peaks are avoided.
Which tests are suitable for approval without specific standard specifications?
Representative impact and pressure/suction tests, leak testing, temperature changes, visual inspection and dimensional control. The test parameters are derived from the project-specific load collective and documented.