Polybutylene terephthalate plastic
PBT (polybutylene terephthalate) stands out for its high strength, chemical resistance & electrical insulation. Production & areas of application.
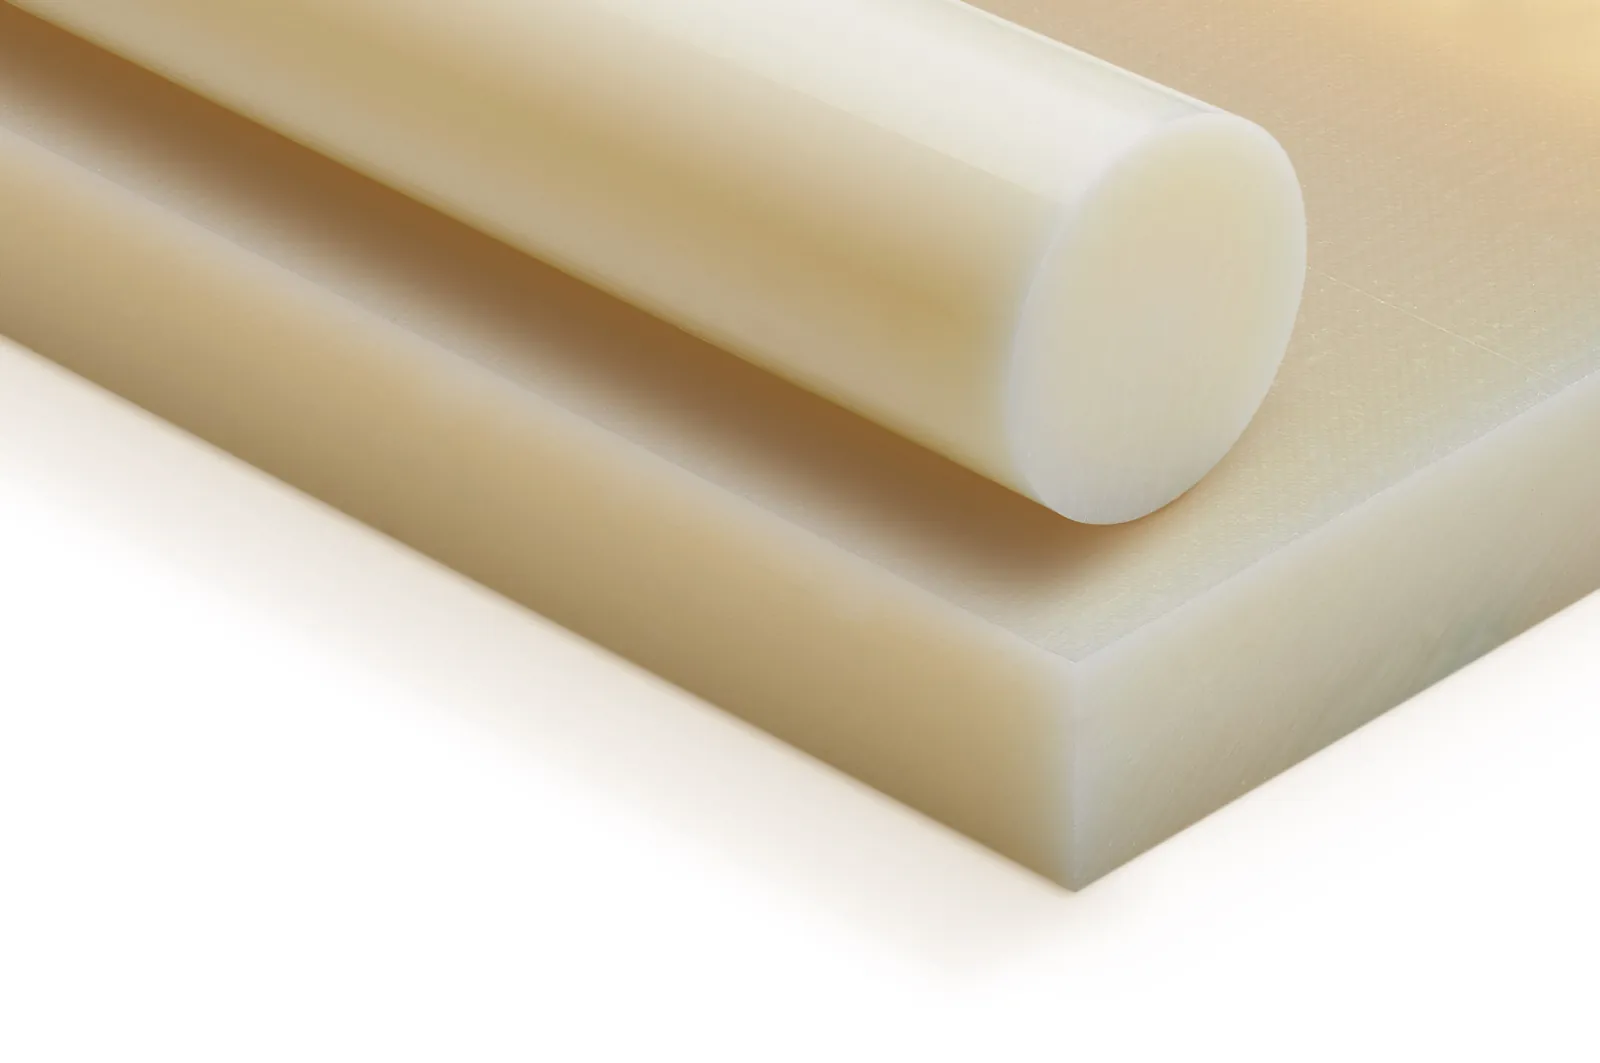
PBT plastic, spelled out as polybutylene terephthalate, is a semi-crystalline thermoplastic polyester for dimensionally accurate and technically demanding components. The material combines low moisture absorption with good electrical insulation properties, high stiffness, good chemical resistance and economical processability.
PBT is particularly frequently used for connectors, switches, sensor components, bobbins, housings and components in vehicle construction. Depending on the requirement, unreinforced, glass-fibre-reinforced, flame-retardant, impact-modified and hydrolysis-stabilised PBT types are available.
Martan Plastics supports industrial companies in selecting suitable plastic materials and in manufacturing application-specific components.
What is PBT?
PBT belongs to the material group of thermoplastic polyesters. It is produced by the polycondensation of terephthalic acid or corresponding starting compounds with 1,4-butanediol.
The plastic has a semi-crystalline material structure. This influences, among other things, stiffness, strength, chemical resistance, shrinkage and heat deflection temperature. In contrast to amorphous plastics, PBT has a defined melting range and in unreinforced form is usually not transparent.
Rapid crystallisation is a key advantage in processing. It enables short moulding and cooling times, which is why PBT is particularly suitable for economical series production in plastic injection moulding.
The most important properties of PBT plastic
PBT is used when a component must remain dimensionally accurate and functional even under changing moisture, elevated temperatures or contact with operating media. However, the specific property profile depends strongly on the particular PBT type, possible reinforcing materials and the processing conditions.
Low water absorption
A decisive advantage of PBT is its low water absorption compared with many polyamides. As a result, dimensions and mechanical properties change only comparatively little under changing humidity.
This moisture stability is particularly important for components with tight tolerances, precise snap-fit connections, electrical contact spacings or defined fits. Typical examples are connectors, sensor housings, bobbins and switching elements.
High dimensional accuracy
The low moisture absorption and the comparatively high stiffness enable good dimensional stability. PBT is therefore suitable for precision components whose function depends on reproducible dimensions.
With glass-fibre-reinforced types, stiffness and heat deflection temperature increase significantly. At the same time, fibre orientation can cause direction-dependent shrinkage and warpage. The component geometry, gate position and mould design must therefore be matched to the particular material type.
Good mechanical strength and stiffness
Unreinforced PBT offers a balanced ratio of stiffness, strength and toughness. Glass-fibre-reinforced variants, for example PBT GF30, achieve substantially higher strength and stiffness values and are therefore suitable for structural parts subject to greater mechanical stress.
At low temperatures or pronounced notches, however, PBT can react more brittlely. Sharp transitions, unfavourable wall thickness jumps and high local stresses should therefore be avoided in the design.
Good electrical insulation
PBT has good dielectric properties and retains them comparatively stably due to its low moisture absorption. The material is therefore frequently used for components in the electrical industry and electronics.
Depending on the material type, high comparative tracking indices, good dielectric strengths and flame-retardant versions are available. For safety-relevant applications, the specific material approval, the required UL classification, wall thickness and component geometry must be checked.
Good chemical resistance
PBT is resistant to numerous oils, greases, fuels, alcohols and many organic solvents. The material is therefore suitable for components that come into contact with lubricants, cleaning media or operating fluids.
Limitations exist, among other things, with respect to strong alkalis, certain hot aqueous media and prolonged hydrolytic exposure. For humid and thermally stressed environments, specially hydrolysis-stabilised PBT types are available.
The actual resistance should always be assessed on the basis of the specific chemical, concentration, temperature, exposure duration and mechanical load.
Good surface quality
PBT enables clean surfaces in injection moulding and the precise reproduction of fine geometries. This is advantageous, for example, for visible housing parts, plug contours, snap-fit lugs and small functional elements.
Typical technical characteristic values of PBT
The following table shows guide values for unreinforced and technically modified PBT types. It does not replace a material-specific data sheet. Glass fibre content, additives, conditioning, test method and processing conditions can significantly change the values.
| Property | Typical guide range | Typical test standard |
|---|---|---|
| Density | approximately 1.30 to 1.35 g/cm³ | ISO 1183 |
| Melting temperature | approximately 220 to 230 °C | ISO 11357 |
| Tensile strength, unreinforced | often approximately 50 to 65 MPa | ISO 527 |
| Modulus of elasticity, unreinforced | often approximately 2,000 to 2,800 MPa | ISO 527 |
| Water absorption after 24 hours | often approximately 0.1 to 0.2 % | ISO 62 |
| Processing shrinkage, unreinforced | often approximately 1.5 to 2.5 % | type-dependent |
| Heat deflection temperature | strongly dependent on load and reinforcement | ISO 75 |
| Comparative tracking index | dependent on type and additives | IEC 60112 |
Important: Heat deflection temperature and permissible continuous service temperature must not be equated. The heat deflection temperature describes the behaviour of a standardised test specimen under a defined load. The permissible service temperature of a real component additionally depends on load, duration of use, geometry, environment and material ageing.
Temperature resistance of PBT
The temperature resistance of PBT depends strongly on the material type used. Unreinforced PBT and glass-fibre-reinforced PBT can exhibit significantly different mechanical behaviour at elevated temperature.
Continuous service temperature
For many PBT types, long-term service temperatures in the range of approximately 100 to 130 °C are specified. Specially stabilised or reinforced types can also be used above this depending on the application. However, a blanket approval up to 140 °C is not reliable without checking the specific material data sheet.
In the design, in addition to the ambient temperature, mechanical loads, exposure duration, temperature cycles, air supply, moisture and chemical media must be taken into account in particular.
Heat deflection temperature
Glass-fibre-reinforced PBT types achieve a significantly higher heat deflection temperature than unreinforced variants. As a result, they can be used for dimensionally stable housings, supports, mounts and plug-in systems in thermally stressed areas.
However, high values from a data sheet apply exclusively to the specified test method, load and specimen geometry. They cannot be directly adopted as the maximum permissible component temperature.
Temperature cycling
PBT is fundamentally suitable for components that are repeatedly heated and cooled. In the design, the thermal expansion of the plastic, adjacent materials and possible stress peaks must be taken into account.
In metal-plastic connections, different coefficients of thermal expansion can lead to additional loads. Suitable tolerances, flexible mounting points and low-stress geometries increase operational reliability.
Electrical properties and fire protection
The combination of electrical insulation, low moisture absorption and good dimensional accuracy makes PBT an important material for electrical and electronic components.
Typical applications are:
- plugs and connectors
- switch housings
- terminal blocks
- bobbins
- relay carriers
- fuse components
- sensor carriers
- housings for control and power electronics
For applications with fire protection requirements, flame-retardant PBT grades are available. Depending on the type, classifications such as UL 94 V-0 can be achieved. However, the classification applies only to defined material thicknesses and the particular tested material formulation.
The comparative tracking index is also type-dependent. A specific CTI value should therefore not be generalised, but taken from the data sheet of the intended PBT grade.
PBT in injection moulding
PBT is primarily processed by injection moulding. The good flowability enables the production of thin-walled components, delicate contours and complex functional geometries. Rapid crystallisation supports short cycle times and economical series production.
Drying before processing
PBT is not very moisture-sensitive in later use, but must be carefully dried before melt processing. Excessive residual moisture can lead to hydrolytic degradation of the polymer chains during processing. This can impair strength, toughness and surface quality.
Drying temperature, drying duration and permissible residual moisture depend on the respective manufacturer's data sheet. Blanket specifications should not be applied to all PBT types.
Processing temperature
The melt temperature for many PBT types is approximately between 240 and 260 °C. The suitable mould temperature depends on the material type, component geometry, surface requirement and desired degree of crystallisation.
Too low a mould temperature can impair surface quality and crystallisation. Excessive thermal load or long residence time, on the other hand, can lead to material degradation.
Shrinkage and warpage
As a semi-crystalline plastic, PBT exhibits higher processing shrinkage than many amorphous thermoplastics. For unreinforced types, it can often be in the range of approximately 1.5 to 2.5 per cent.
Glass fibres reduce shrinkage but lead to greater direction-dependence. Fibre orientation along the flow paths can cause different longitudinal and transverse shrinkage. Material-appropriate mould and component design is therefore crucial.
Design notes for PBT components
So that PBT can reliably exploit its properties in the component, some basic principles should be taken into account already during design.
- design wall thicknesses as uniformly as possible
- avoid abrupt wall thickness jumps
- sufficiently round transitions and internal corners
- dimension ribs and bosses in a material-appropriate way
- take shrinkage and possible fibre orientation into account
- reduce notch stresses at snap-fit lugs and mounting points
- integrate metal inserts with low stress
- define temperature and moisture conditions realistically
- determine necessary comparative tracking and fire protection classes at an early stage
For highly stressed components, a component-specific test is recommended. Data sheet values are determined on standardised test specimens and only inadequately reflect complex geometries, weld lines, ageing and real load combinations.
PBT GF30 and other modified PBT types
Through reinforcements and additives, the property profile of PBT can be specifically adapted to different applications.
PBT GF30
PBT GF30 generally contains around 30 per cent glass fibres. Compared with unreinforced PBT, the material offers significantly higher stiffness, strength and heat deflection temperature. At the same time, shrinkage and thermal expansion decrease.
A lower elongation at break, higher notch sensitivity, anisotropic properties and greater mould wear during processing must be taken into account.
Flame-retardant PBT
Flame-retardant PBT variants are used for connectors, switches, bobbins and other electrical components. Depending on the formulation and wall thickness, different fire protection classifications are available.
Hydrolysis-stabilised PBT
Hydrolysis-stabilised types are intended for components that are simultaneously exposed to moisture and elevated temperatures over a prolonged period. Typical areas of use are found in vehicle construction, in sensors and in electrical plug-in systems.
Impact-modified PBT
Impact-modified variants reduce the tendency to brittle fracture and are suitable for components that must withstand impact loads, assembly forces or low temperatures.
PBT blends
PBT can be combined with other polymers. Such blends are used, for example, to specifically influence impact toughness, warpage, surface quality or processing behaviour. The properties of a blend can differ significantly from those of a pure PBT.
Typical applications of PBT plastic
Electrical engineering and electronics
In electrical applications, PBT benefits from its low water absorption, good insulation and high dimensional accuracy. The material is used, among other things, for connectors, terminal strips, switches, relay bases, bobbins and housings.
Vehicle construction
In vehicle construction, PBT is used, among other things, in plug-in systems, sensors, actuator housings, lighting components and components in the engine compartment. For areas with moisture and heat, hydrolysis-stabilised and glass-fibre-reinforced types are frequently used.
Mechanical and plant engineering
In mechanical and plant engineering, PBT is suitable for dimensionally accurate housings, supports, covers, functional elements and electrically insulating components. For parts subject to heavy sliding or abrasive stress, however, other engineering plastics may be more suitable.
Household and appliance technology
PBT is used in household appliances and technical devices, for example, for switch components, plug-in systems, fan parts, housings and temperature-stressed structural elements.
Sensor technology and automation
The dimensional accuracy and electrical properties make PBT interesting for sensor holders, sensor housings, plug contacts and components of automated systems. In the case of direct media contact, the chemical resistance must be checked for the specific application.
PBT or PA – which plastic is more suitable?
PBT and PA plastic are frequently used for technically stressed components, but differ significantly in their moisture and wear behaviour.
| Criterion | PBT | PA 6 or PA 66 |
|---|---|---|
| Water absorption | low | significantly higher |
| Dimensional accuracy under moisture | very good | more strongly moisture-dependent |
| Electrical properties | comparatively moisture-stable | more strongly influenced by moisture |
| Wear and sliding properties | good, type-dependent | often better |
| Toughness | type-dependent, sometimes notch-sensitive | often higher |
| Injection moulding processing | rapid crystallisation | well established, type-dependent |
PBT is often the better choice when dimensional accuracy, electrical insulation and low moisture absorption are the priority. PA can be advantageous when high toughness, dynamic load capacity or pronounced wear properties are required.
PBT or PET – the differences
PBT and PET plastic both belong to the thermoplastic polyesters. However, their chemical relationship does not mean that they are interchangeable in every application.
| Criterion | PBT | PET |
|---|---|---|
| Crystallisation behaviour | faster | slower |
| Injection moulding cycle time | often shorter | more strongly dependent on process control |
| Dimensional accuracy | very good | very good |
| Stiffness | high | often somewhat higher, type-dependent |
| Impact toughness | often more favourable | often more notch-sensitive |
| Typical technical use | plugs, housings, sensor technology | precision and wear parts, technical semi-finished products |
PBT is particularly frequently used for complex injection-moulded parts in large quantities. Technical PET can offer advantages in stiffness, hardness, creep behaviour and mechanically precise components. The specific requirement profile is decisive.
PBT or POM?
PBT and POM plastic both have low water absorption and good dimensional accuracy. POM often offers better sliding and wear properties as well as high resilience. PBT, on the other hand, is advantageous for many electrical applications and is available in numerous flame-retardant or glass-fibre-reinforced variants.
For gears, bearings and moving precision parts, POM may be more suitable. For connectors, bobbins and electrically insulating housings, PBT is often preferred.
Advantages and limits of PBT
| Advantages | Limits to be taken into account |
|---|---|
| low water absorption | drying required before melt processing |
| good dimensional accuracy | semi-crystalline processing shrinkage |
| good electrical insulation | properties strongly dependent on the material type |
| good chemical resistance | sensitive to certain alkalis and hydrolysis conditions |
| rapid crystallisation | notch sensitivity with unfavourable design |
| short injection moulding cycles | possible warpage with fibre-reinforced types |
| numerous modified variants | no blanket temperature or fire protection approval |
When is PBT the right material choice?
PBT is particularly suitable when several of the following requirements must be met simultaneously:
- low dimensional change under changing humidity
- good electrical insulation
- precise and complex injection moulding geometries
- short cycle times in series production
- contact with oils, greases or fuels
- increased stiffness through glass fibre reinforcement
- flame-retardant material version
- good surface quality
- thermally stressed housings and supports
PBT, on the other hand, is not automatically the best choice for permanently hot water environments, extreme impact loads, heavily sliding components or applications above the type-dependent temperature range. In these cases, alternatives such as POM, PA, PET, PPS, PEI or PEEK should be considered.
PBT components and material selection with Martan Plastics
The selection of the suitable PBT type does not depend on the material name alone. The actual operating conditions and the required component properties are decisive.
For a reliable material and production recommendation, the following information is particularly helpful:
- component drawing or CAD data
- dimensions and tolerances
- mechanical load
- continuous and peak temperatures
- contact with moisture or chemicals
- electrical requirements
- fire protection and approval requirements
- desired quantity
- surface and colour requirements
Martan Plastics supports you in selecting suitable engineering plastics and in implementing application-specific plastic components for industrial areas of use.
FAQ on PBT plastic
What does PBT mean in plastics?
PBT stands for polybutylene terephthalate. It is a semi-crystalline thermoplastic polyester that is used primarily for dimensionally accurate electrical and technical components.
Is PBT a thermoplastic?
Yes. PBT is a thermoplastic plastic. It becomes mouldable when heated sufficiently and can be processed, among other things, by injection moulding.
How temperature-resistant is PBT?
The permissible service temperature depends on the particular PBT type, load and duration of use. For many types, the long-term service range is approximately between 100 and 130 °C. Reinforced or specially stabilised variants can meet higher requirements.
Is PBT waterproof?
PBT absorbs only a little water and therefore remains comparatively dimensionally accurate under changing humidity. However, standard PBT is not indefinitely resistant to permanent contact with hot water or high humidity at elevated temperature. Hydrolysis-stabilised types may be required for this.
Does PBT need to be dried before injection moulding?
Yes. PBT must be carefully dried before melt processing. Residual moisture can cause hydrolytic material degradation at high processing temperature. The specific drying parameters depend on the material data sheet.
What is PBT GF30?
PBT GF30 is a PBT reinforced with approximately 30 per cent glass fibres. The reinforcement increases in particular stiffness, strength and heat deflection temperature and reduces processing shrinkage.
Is PBT suitable for electrical components?
Yes. PBT is frequently used for connectors, switches, bobbins and housings. For specific applications, the dielectric strength, comparative tracking index, fire protection class and required approvals of the particular material type must be checked.
What is the difference between PBT and PA?
PBT absorbs significantly less moisture and therefore remains more dimensionally accurate. Depending on the type, PA often offers higher toughness and better wear properties. The choice depends on the application.
What is the difference between PBT and PET?
PBT crystallises faster and can therefore often be injection-moulded with shorter cycle times. PET can offer advantages with regard to stiffness, hardness and creep behaviour in certain technical applications.
Is PBT chemical-resistant?
PBT is resistant to many oils, greases, fuels and solvents. Nevertheless, suitability must be checked for the specific medium, its concentration, temperature and exposure duration.